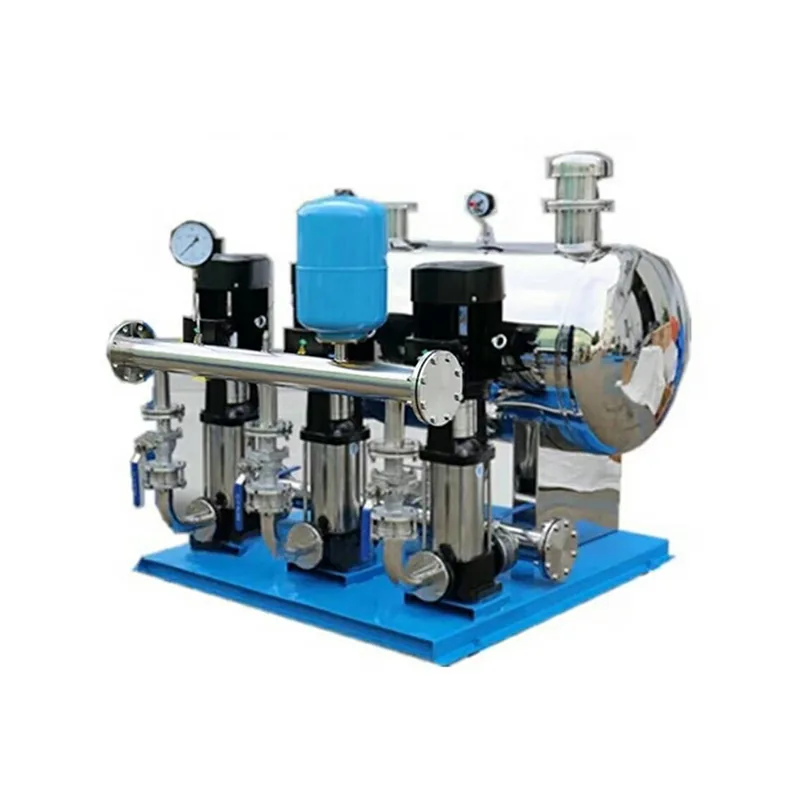
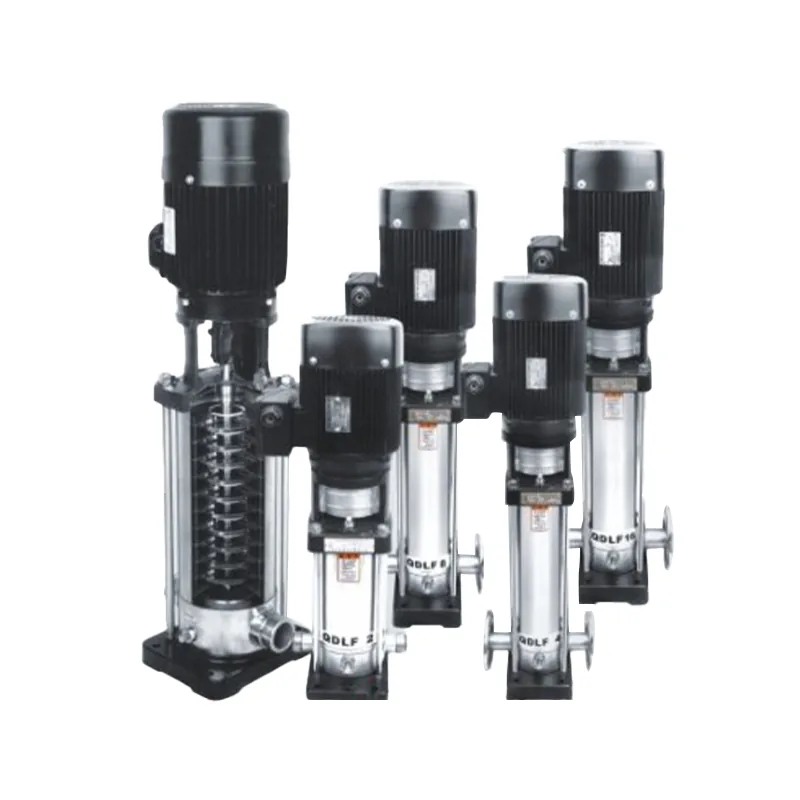
Horizontal multistage centrifugal pumps represent a versatile and robust class of fluid-handling equipment designed for industrial, commercial, and municipal applications requiring reliable high-pressure liquid transfer. Engineered with a horizontally aligned shaft configuration and multiple impellers mounted in series, these pumps are optimized to deliver sustained performance in demanding environments. Their modular design allows for scalability, enabling customization to meet specific flow rate and pressure requirements across diverse industries. Key features of this category include compact footprint, high operational efficiency, and adaptability to variable system demands.
The operating principle of horizontal multistage centrifugal pumps relies on sequential energy transfer through successive impellers. Each stage incrementally increases the liquid’s velocity and pressure, culminating in a cumulative output suitable for tasks such as boiler feed, water supply networks, chemical processing, and HVAC systems. Unlike single-stage alternatives, this configuration maintains efficiency across extended pressure ranges while reducing shaft deflection and vibration. Key design elements, including durable casings and precise impeller alignment, ensure consistent performance and reduced mechanical wear over time.
Applications span a wide spectrum of sectors. In power generation, they support cooling water circulation and boiler feed systems. The oil and gas industry utilizes these pumps for pipeline transport, refinery operations, and enhanced oil recovery. Water treatment facilities employ them for distribution, filtration, and reverse osmosis systems. Additionally, chemical manufacturers rely on their corrosion-resistant materials and sealing systems to handle aggressive media safely. Municipal projects often feature these pumps for potable water delivery and wastewater management.
Design versatility enhances their usability. Horizontal orientation facilitates easier maintenance and inspection, as components are accessible from the installation plane. Modular construction permits the addition or removal of stages to align with changing operational needs. Various seal options—such as mechanical seals or gland packing—enable compliance with fluid-specific integrity standards. Shaft materials, impeller coatings, and casing linings further extend suitability for handling abrasives, high-viscosity fluids, or elevated temperatures.
These pumps integrate seamlessly with automated control systems, supporting variable frequency drives to optimize energy consumption while maintaining operational flexibility. Their relatively low noise levels and vibration resistance make them suitable for noise-sensitive environments. Long service intervals and reduced maintenance requirements contribute to operational cost savings, while standardized spare parts availability reduces downtime.
Zhejiang MingYuan Pump Co., Ltd. is located in Liangshan Industrial Zone, Daxi Town, Wenling City, the "hometown of water pumps", close to National Highway 104 and National Highway G15, at the Daxi exit. The company is a professional China Submersible Pump manufacturer and wholesale Submersible Pump factory integrating scientific research, design, production, and sales online. The company has always been committed to innovation in technology and management, and has developed water pumps suitable for industrial and mining enterprises, construction sites, urban water supply, farmland irrigation and drainage, high-rise building water supply, fire protection, industrial water treatment, sewage treatment,t and other industries based on market demand. The company's leading products include: 3SDM, 3.5SDM, 4SDM, YQJD series stainless steel deep well pumps; QGD series screw submersible pumps; QXD, QD series small submersible pumps; QY series oil-immersed submersible pumps; WQD, WQ series sewage and sewage submersible pumps; WQV, WQK series cutting sewage and sewage submersible pumps; WZB, QB, CPM, DTM, JET series land pumps; RG, ISG, SGR, SG series pipeline pumps, etc. The company has successively obtained the national industrial product production license, agricultural machinery promotion license, and obtained IS09001: 2015 quality management system certification.
Founded in
Factory area
Export ratio
Number of employees
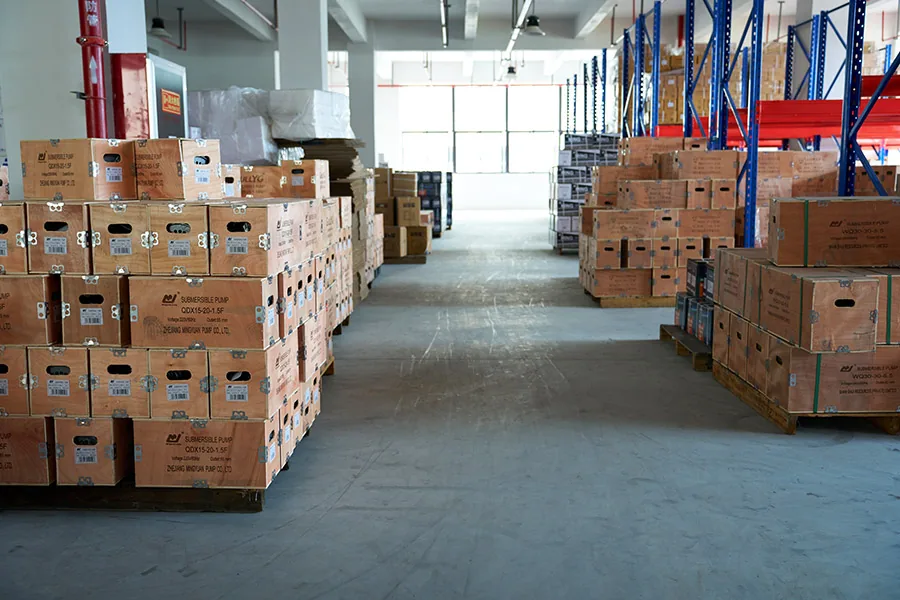
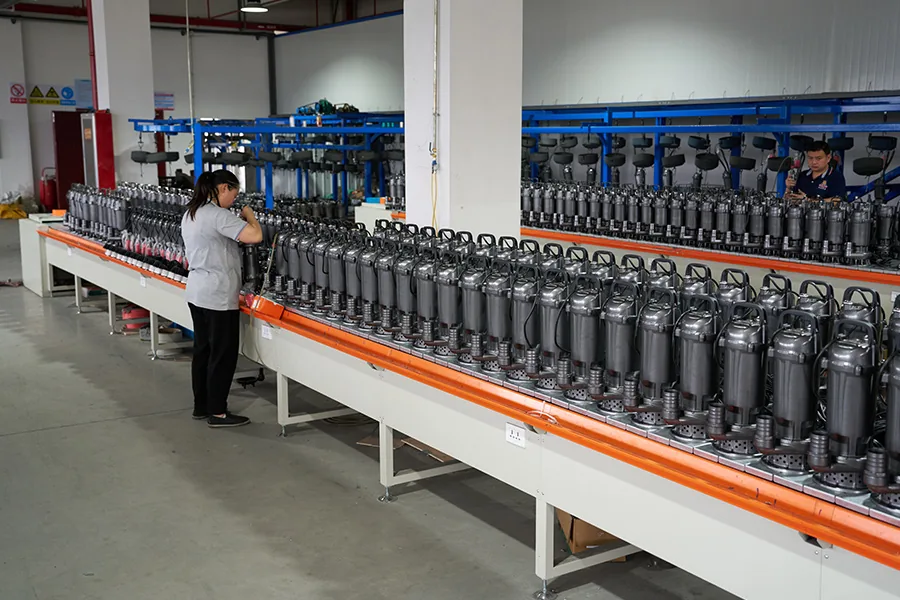
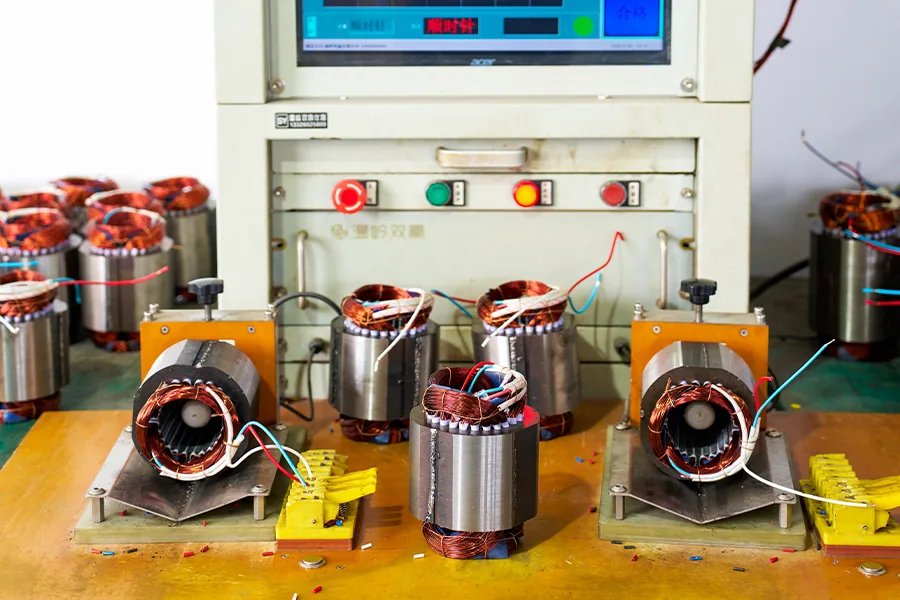
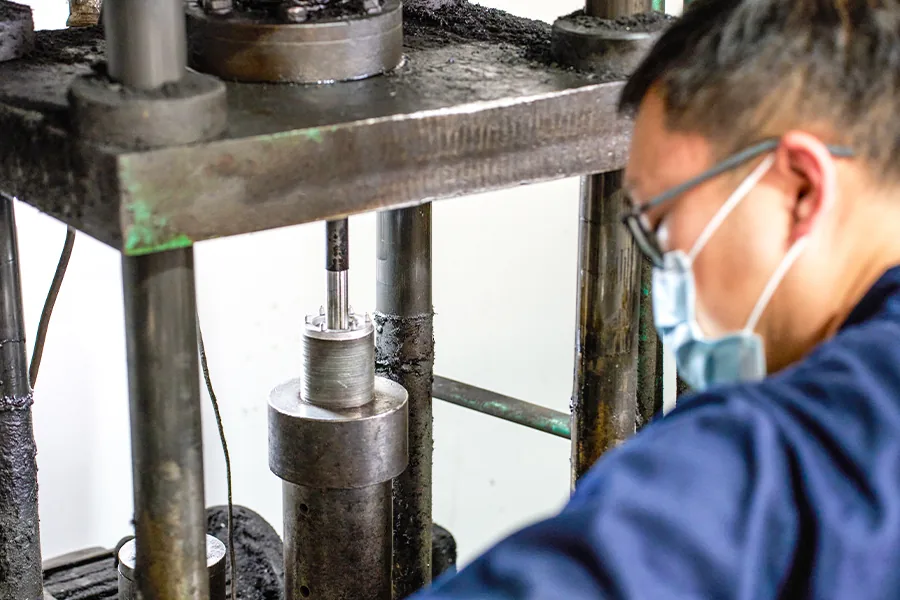
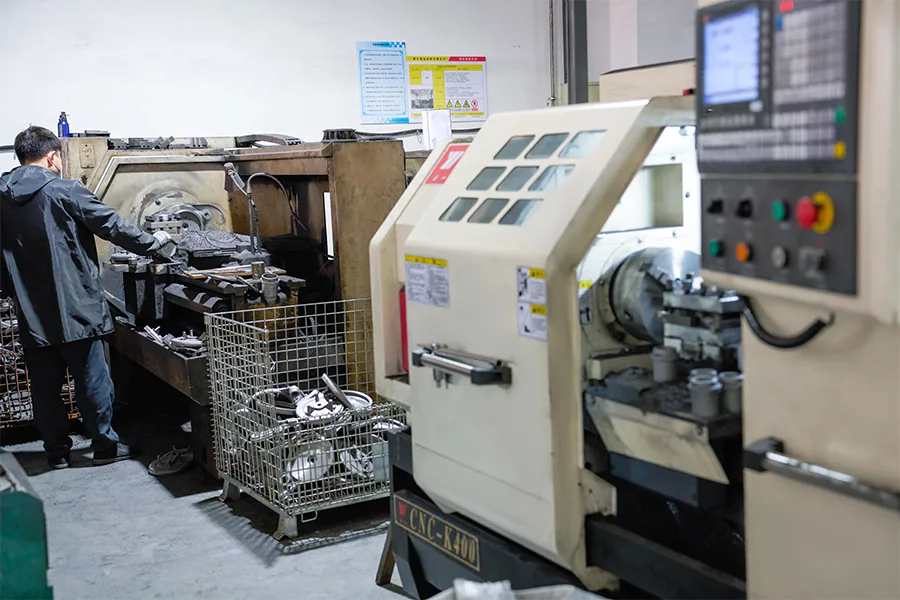
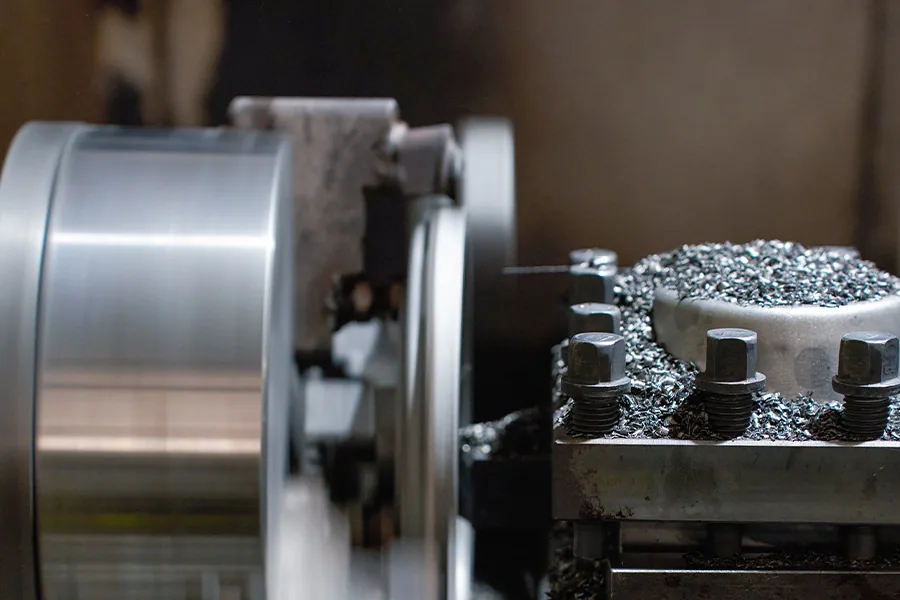
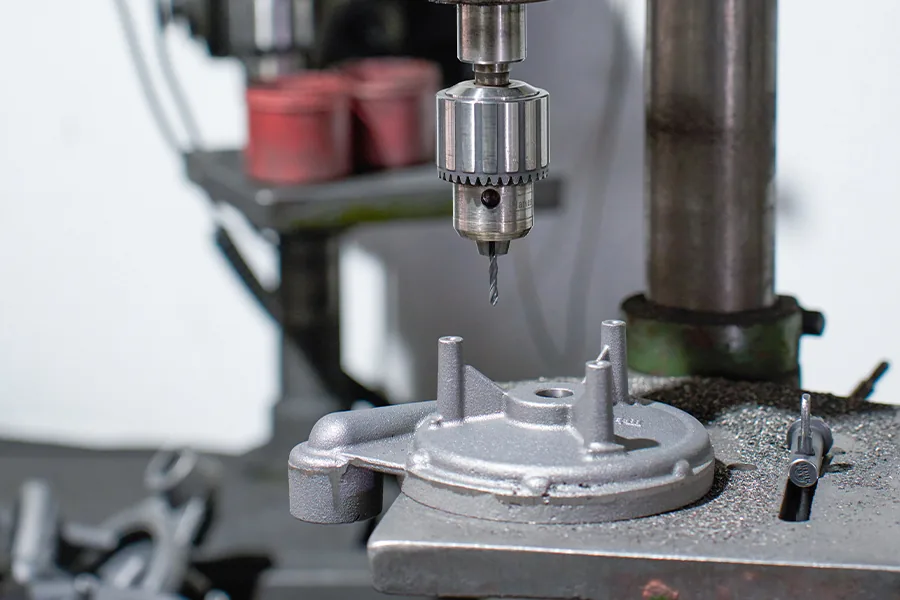
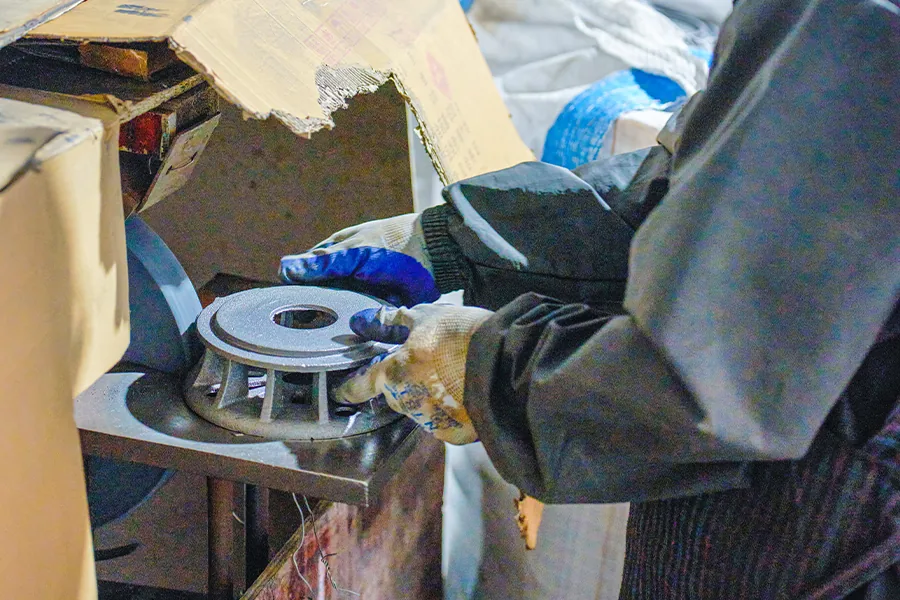
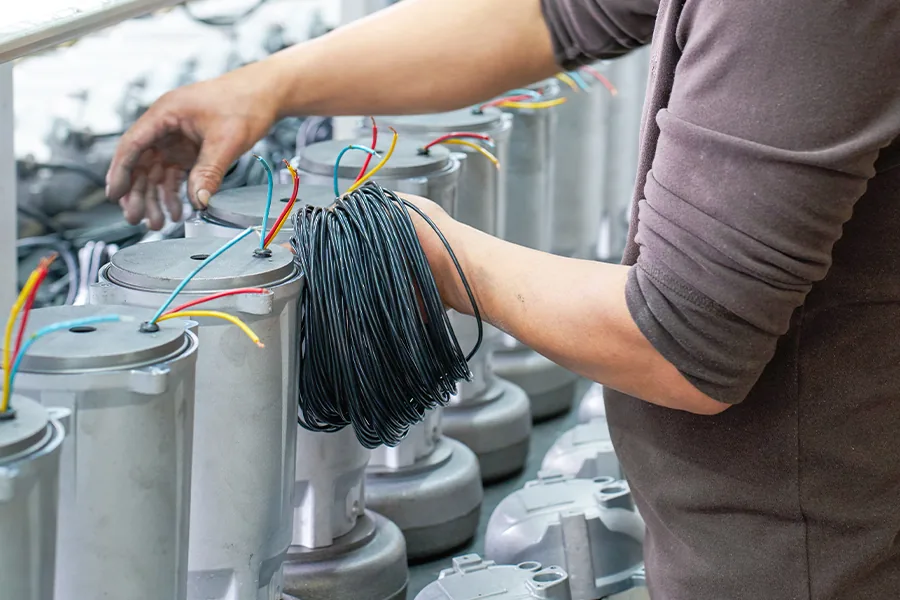
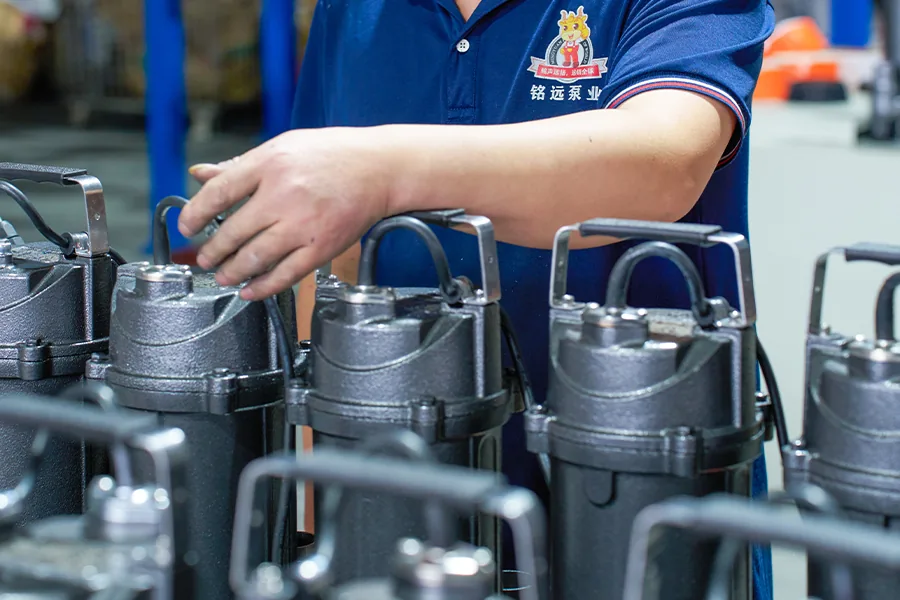
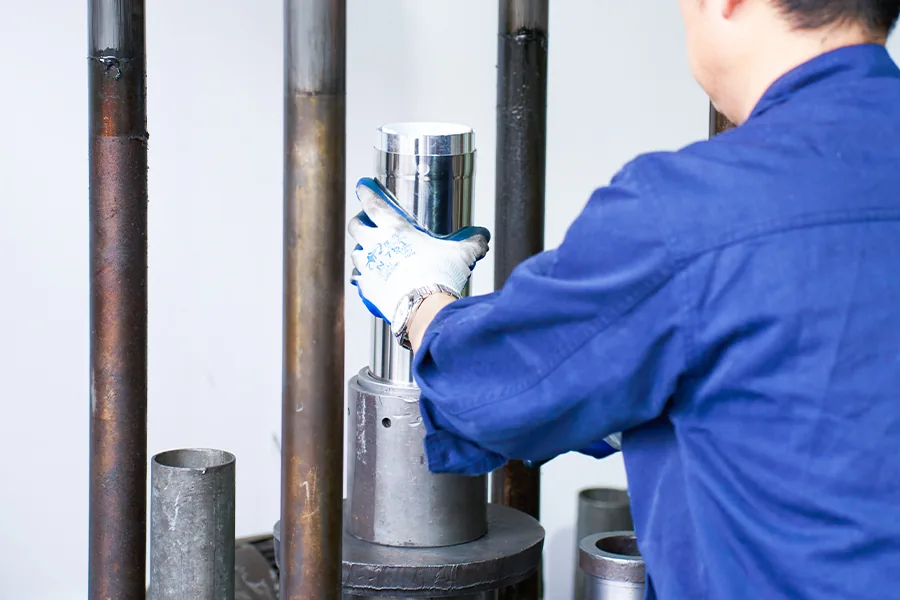
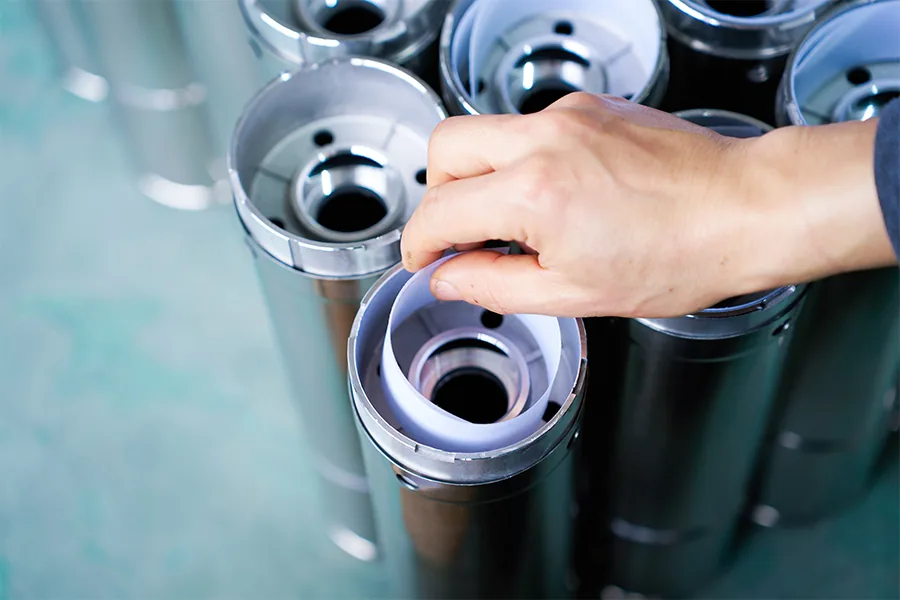
The company continues to upgrade and optimize workshop equipment in order to produce products that satisfy customers.
Wastewater systems in demanding environments require pumps that withstand severe...
View MoreOff-grid water supply solutions increasingly rely on solar energy. Remote irriga...
View MoreSubmerged pumping applications demand equipment that performs flawlessly underwa...
View MoreWastewater systems depend on reliable pumping equipment. Municipal treatment pla...
View MoreWater access defines agriculture and rural living. Irrigation. Livestock. Drinki...
View MoreSewage pumps move dirty water. They handle solids. They run submerged. They work...
View MoreThe submersible pump industry plays a vital role in sectors such as agriculture, construction, sewage treatment, and residential water supply. As demand for efficient and reliable fluid handling systems continues to grow, more users are turning to advanced solutions provided by a high efficiency submersible pump supplier.
A submersible pump is a device designed to operate while fully submerged in the fluid it is intended to move. It typically consists of a sealed electric motor and an impeller system enclosed in a waterproof casing. These pumps are used in applications ranging from draining floodwater and emptying tanks to supplying clean water from wells and handling wastewater in municipal systems.
The compact design and submersion capability of the submersible pump help prevent air-lock issues and allow for efficient vertical lifting of liquids. This makes it suitable for deep well applications, as well as for use in limited-space environments such as basements or narrow boreholes.
A high efficiency submersible pump supplier provides pump solutions that are engineered for reduced energy consumption and stable performance. These suppliers focus on design improvements such as advanced motor technology, precision-balanced impellers, and corrosion-resistant materials to support long-term usage with little power waste.
Choosing a high efficiency submersible pump supplier helps businesses and homeowners lower operating costs over time. These suppliers often offer a wide range of models suited for various flow rates and pressure requirements, enabling customers to select a pump that fits their actual usage conditions.
Behind every quality submersible pump is a factory equipped with the tools and systems to carry out material processing, motor assembly, quality inspection, and performance testing. A capable factory can produce a wide range of pump types, including clean water pumps, sewage pumps, and deep well submersibles.
A submersible pump factory typically manages the full manufacturing process—from casting and machining components to assembly and waterproof sealing. Factories that emphasize structured production and testing protocols are better positioned to deliver pumps that meet consistent performance expectations.
Some high efficiency submersible pump suppliers operate their own factories, while others partner closely with certified manufacturers. Either way, the factory's role ensures that each submersible pump is built to required tolerances and can handle demanding environments.
Many factories and suppliers offer submersible pump OEM service, which allows clients to request customized designs and specifications based on their application needs. OEM (Original Equipment Manufacturer) service is commonly used by project contractors, distributors, and private-label brands seeking unique pump features or customized branding.
Through submersible pump OEM service, buyers can specify adjustments in pump housing materials, impeller size, motor wattage, voltage compatibility, and even packaging. This service is particularly useful in large projects where system integration, performance consistency, or local compliance is required.
A high efficiency submersible pump supplier that provides OEM service adds further value by helping customers select pump configurations that reduce energy use while still meeting system goals.
The submersible pump industry combines technical design, factory precision, and application knowledge to provide solutions for a wide range of fluid handling tasks. A reliable high efficiency submersible pump supplier contributes to energy savings, stable operation, and product adaptability—especially when paired with factory support and OEM service. By understanding how these roles function within the industry, buyers can make more informed decisions that support both performance and long-term value.
 English
 Español
 العربية